

The joint feels hot, the solder is touching the copper, and it just sits there in a ball. Or it runs onto the outside of the fitting and refuses to pull into the cup. I work through water, surface preparation, flux and heat before I blame the solder. A hot-looking joint is not proof that both mating surfaces are ready.
Before you light a torch. Clear anything that can burn from behind the joint, or cover it with a flame-protector cloth or a metal heat shield made for soldering. A wet rag is not a heat barrier. Keep a fire extinguisher in reach, and stay and watch the area after the last joint, because framing and insulation can smolder after the flame is out. If the building or the job calls for a hot work permit or a fire watch, get it before you start. [6]
The five causes, in the order they actually happen
- Water in the line. The first condition I check. Water removes heat from the working joint. I drain and isolate it before soldering rather than adding more flame.
- The copper is not clean. Oxide is not a cosmetic problem. Solder wets bright copper and refuses dull copper.
- No flux, not enough flux, or flux that burned off before you got the solder there.
- Heating the wrong place. Heat the joint, not the solder. Warm the tube next to the fitting, then put most of the heat on the fitting body so both reach temperature together.
- Not enough heat for the mass. A larger fitting or valve changes the heating task. I choose a suitable torch and heat both mating parts evenly, following component instructions.
Sources for these checks: [1]
Water, the one that beats everyone
If water keeps reaching the joint, I solve that before changing flux or adding heat. I isolate the supply, open an appropriate low outlet and a high fixture to let the line drain, and check that the shutoff actually holds. If I cannot establish a dry working joint, I choose a listed mechanical connection suitable for that pipe and service.
- Drain it properly: open the lowest fixture and a high one to break the vacuum.
- I skip the bread trick. I prefer keeping foreign material out of a drinking-water line and solving the drainage problem or changing the joining method.
- If the shutoff does not hold, I arrange proper isolation. I do not try to solder a new valve into flowing water. A suitable mechanical connection is another option.
If steam is coming out of the joint, stop. You are not going to solder it. Solve the water first.
Sources for these checks: [1]
Clean means bright, not “looks fine”
I clean both mating surfaces: the outside of the tube and the inside of the fitting cup. The cup is easy to miss, but solder needs to wet that surface too. I use sand cloth, an abrasive pad or a correctly sized fitting brush, then apply flux promptly. I avoid touching cleaned copper with bare hands or oily gloves.
A new fitting still needs its joint surfaces cleaned before assembly. I remove oxidation and surface contamination rather than assuming a fitting is ready because it came straight from a box. I abrade lightly: removing too much copper can leave a loose fit and interfere with the capillary space.
I also ream the cut end to the full inside diameter and remove the outside burr. The Copper Development Association explains that an internal burr can create local turbulence and erosion-corrosion. I remove the shavings before assembly; see the guide to deburring tools for copper pipe for tool choices.
Sources for these checks: [1]
Cleaning and reaming are not tips, they are the specification
Preparation is part of the joining procedure, not an optional finishing touch. The Copper Development Association sets out the ASTM B828 sequence: measure and cut, ream, clean, apply flux, assemble and support, heat, apply solder, cool and clean, then test. I follow that sequence rather than trying to rescue a poorly prepared joint with more heat. [1]
Georgia currently adopts the 2024 International Plumbing Code with state amendments. I check the applicable local requirements and use solder and flux suitable for drinking-water service. The CDA handbook identifies ASTM B32 solder alloys and ASTM B813 flux, and explains the drinking-water restriction on solder containing more than 0.2% lead. NSF's drinking-water listing includes Oatey H-20 95 tinning flux; an electrical or sheet-metal flux is not an interchangeable choice. [1] [3] [5]
Flux does the work you think the torch is doing
Flux helps remove residual oxide, protects the cleaned surfaces from reoxidation during heating and promotes wetting. It complements mechanical cleaning rather than replacing it. I brush on a thin, even film on the tube and fitting; I do not apply it with my fingers or pack the cup with paste.
- Oatey H-20 95 tinning flux contains solder powder to pre-tin the pipe. I use it on clean copper and still check the joint temperature, rather than expecting the paste to cure every flow problem.
- Oatey 22017 95/5 lead-free solder is the maker's bulk 1 lb spool example. Its catalog identifies a tin-antimony alloy for plumbing. For solder and flux options, I use the separate copper-pipe guide rather than choosing by spool size alone.
More flux is not better. Excess residue can cause corrosion, so I remove exterior excess after assembly, let the finished joint cool naturally, then clean it. I flush the completed system as its service and the manufacturer's instructions require, before returning it to use. I never treat flushing as a way to excuse a thick layer of flux inside the joint.
The wider comparison of pastes and alloys is in solder and flux for copper pipe.
Heat the joint, and let it pull the solder
For an ordinary copper tube and fitting joint, I begin by preheating the tube around its circumference, then move onto the fitting cup and sweep between the cup and tube. Both parts need to reach soldering temperature. A valve is a separate case: I follow its own instructions for heat placement, position and protection of heat-sensitive parts.
Test with the solder, not with your eyes. Touch the wire to the joint away from the flame. If it melts on contact with the metal, the joint is ready and capillary action will pull it all the way around and against gravity. If it does not melt, take the solder away and give it more heat; do not melt the wire in the flame and drip it on. That is how you get a joint that looks soldered and leaks.
Overheating can burn away the flux's effectiveness. If the flux is burned and the joint will not wet, I stop, let the assembly cool and remake the joint with cleaned surfaces and fresh flux. I do not keep cooking it or brush fresh flux onto dangerously hot metal.
A flame that keeps dying mid-joint is a separate problem: see why your torch keeps going out and plumbing torches.
Bernzomatic TS8000 details [4]
More metal changes the heating task. I choose a torch suitable for the tube size, fitting material and work area, and use controlled, even heating instead of simply turning up the flame. Bernzomatic describes the TS8000 family with trigger ignition and a continuous-flame lock. I release that lock and extinguish the flame before setting the torch down, and keep the hot tip away from anything that can burn. [4]
Read the symptom backwards
I use the symptom to choose what to inspect next. It narrows the checks; it does not prove a single cause or establish that the joint is sound:
- Solder balls up and rolls off the metal. No flux where you are touching, or the surface is not clean. Check preparation and joint temperature.
- Solder melts but runs down the outside of the fitting and never enters the cup. The fitting cup may be too cold, or preparation may be incomplete. Move more of the flame onto the fitting body so the whole joint comes up to heat together.
- Solder melts only when it is in the flame. The joint is cold. Take the wire out of the flame entirely and keep heating.
- The joint hisses, spits, or steams. Water. Stop and drain it.
- Everything looked right, but it leaks afterward. Movement during cooling, incomplete filling or poor preparation are possibilities. I remake the connection and test it rather than guessing.
- The flux is black and nothing will wet. I suspect overheated flux, stop heating, let it cool and remake the joint with clean surfaces and fresh flux.
Sources for these checks: [1]
The order the job actually happens
I gather the cutter, reamer, cleaning materials, flux and solder before starting. That keeps the preparation sequence together and avoids handling cleaned surfaces while hunting for tools. I check fit and support before heating, with a plan for draining the line and protecting the surroundings.
- I dry-fit and mark the run first. I confirm the tube seats fully, then complete the cleaned and fluxed joint the same day rather than leaving it unfinished overnight.
- Cut, ream, clean, flux: one joint’s worth at a time, in that order, with no gap between cleaning and fluxing.
- Support the pipe before you light anything. Movement can disturb the joint. I keep the tube and fitting supported as the solder solidifies.
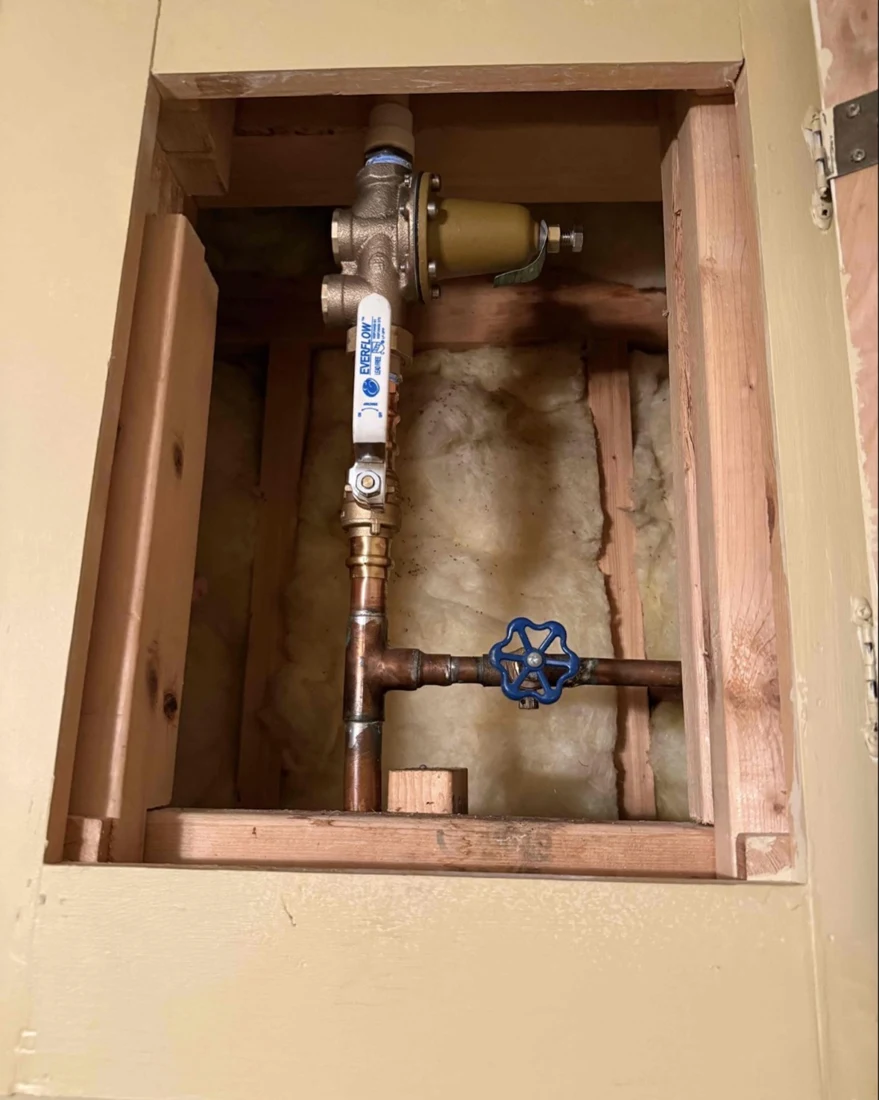
- I drain the line and follow the exact valve instructions for handle position and protection of heat-sensitive parts. I remove components only when the maker directs it. The valve-position guide explains why a universal rule is unsuitable.
- Protect what is behind the joint: a flame-protector cloth or metal heat shield between the flame and joists, insulation, or a finished wall. A soaked rag is not a heat barrier. Have an extinguisher in reach.
- I heat, test with the wire and feed the solder, then let the joint cool naturally without movement. I clean the cooled exterior; I do not quench the joint with a wet rag.
- Flush the line hard before it goes back in service, then pressure-test and look at it again the next day.
Sources for these checks: [1]
When to stop trying
I change method when the working conditions make soldering unsuitable. The CDA handbook identifies mechanical joining as useful where residual water cannot be removed or flame is impractical. The fitting still has to be approved for the exact pipe, size, service and installation location. Damaged or badly thinned tube needs a sound replacement section, not a fitting used to hide the damage. I compare copper press fitting brands separately; ProPress vs soldering and SharkBite vs ProPress explain the two routes.
If I cannot protect nearby combustibles, inspect the hidden side of the work or meet the site's hot-work and fire-watch requirements, I stop. In an occupied building I arrange the work with the responsible person before lighting a torch. A mechanical connection can avoid flame, but it still needs the correct preparation and a leak test. If the shutoff will not hold or access is unsafe, I call a plumber.
Sources for these checks: [1]
FAQ
Sources for these checks: [1]
Why won’t my solder flow into the joint?
I check for water, dirty mating surfaces, missing or burned flux, and uneven or insufficient joint heat. Capillary action works when the prepared tube and fitting can melt the solder themselves. Melting the wire in the flame tells me nothing about the temperature inside the cup.
Can you solder a pipe with water in it?
I do not attempt the joint while water keeps reaching it. Water carries heat away and makes soldering difficult; more torch time is not my solution. I drain and isolate the line, or choose an appropriate mechanical connection. If the work includes a valve, I follow that exact valve's soldering instructions rather than guessing its handle position.
Do I need tinning flux or regular flux?
Both are options when the exact flux is suitable for the pipe and service. Tinning flux includes solder powder to help pre-tin the copper, as Oatey's catalog explains for H-20 95. I still clean both surfaces and heat the joint correctly. Tinning flux cannot dry a wet line or restore burned surfaces. [2]
Why does solder run down the outside of the fitting instead of into it?
I check the whole joint rather than treating runoff as proof that the tube is hotter. A cold fitting cup, contamination, poor fit or damaged flux can prevent the solder from entering. I recheck preparation and use even heating across the assembly, testing against the copper rather than the flame.
Is any plumbing flux fine for drinking water?
No. I select flux intended for potable-water copper work and check the exact product's directions and drinking-water listing. NSF lists Oatey H-20 95 under NSF/ANSI/CAN 61. That listing concerns health effects; it does not make an unsuitable joint or contaminated pipe acceptable. I also use lead-free solder appropriate for the service. [3]
Can I re-solder a joint that already leaked?
I do not assume that adding solder outside a leaking joint repairs the inside. I isolate and drain the line, let the work cool, then inspect the tube and fitting. My repair choice is to remake the connection with sound, freshly prepared surfaces and test it afterward. If I cannot confirm the condition of the old joint, I replace the affected section instead of repeatedly reheating it.
Sources
- [1] Copper Development Association, Copper Tube Handbook, chapters 6 and 7. Preparation, flux, heating, cooling, testing and wet conditions.
- [2] Oatey product catalog, pages 51 and 53. 22017 solder alloy and 30140 H-20 95 tinning flux.
- [3] NSF, drinking-water system component listings. Oatey H-20 95 water-soluble tinning flux.
- [4] Bernzomatic, TS8000T DuraCast 8000 torch features and instructions.
- [5] Georgia Department of Community Affairs, current state minimum construction codes.
- [6] OSHA, welding and hot-work fire prevention precautions.
- [7] CPSC, 2012 Worthington gas-cylinder recall; separate fuel cylinders, not the selected torch head.
Related guides
Related: if the line simply will not dry, that is an argument for a mechanical joint; see can you press a wet line.
Plumber's fit check
- I clean the outside of the tube without removing enough metal to loosen the fit.
- I clean the cup's inside surface too, apply a thin film of flux and seat the tube fully.
- I support the assembly and bring both mating parts to soldering temperature. I follow separate valve instructions where a valve is involved.
Preparation and joining sequence: [1]
If I cannot isolate the line, protect the area or confirm the pipe is sound, I stop and call a plumber.