Press: the tool
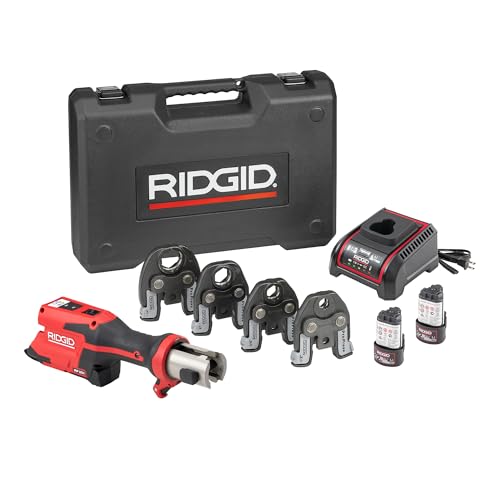
RIDGID RP 251 kit 78148, ½–1¼ in. jaws
at Amazon
Press is fast. Solder costs less to start.
As an Amazon Associate I earn from qualifying purchases. How this site earns
Press for many joints, wet lines or no flame. Solder for the odd repair.
Press: the tool
at Amazon

Solder: the heat
at Amazon

Solder: the flux
at Amazon
Product prices and availability are accurate as of the date/time indicated and are subject to change. Any price and availability information displayed on Amazon.com at the time of purchase will apply to the purchase of this product.
This is where solder surprises people. Done right, a 95/5 soldered joint carries a higher rating on paper than a press joint. These are joint ratings only. The tube, the fittings, the valves on the line, the code and the application all set lower limits, so a joint rating isn’t permission to run or test a system at that pressure.
Press is still rated 300 psi by Viega, so this isn’t a reason to avoid it. It’s a reason not to believe anyone who says solder is the weak joint. The real differences are heat, water in the line, speed and what the tools cost.
| Strengths | Trade-offs |
|---|---|
| No heat or open flame at the joint, per the CDA | The tool kit is a big buy for a few joints |
| Joins wet lines, per Viega | Rated lower than a soldered joint (300 psi Viega, 200 psi general) |
| Four to seven seconds per press, per Viega | Jaws must fit the space around the joint |
| Smart Connect shows an unpressed fitting during the test |
The CDA’s handbook sums up why press caught on: it’s fast, economical and needs no heat or open flame.
The handbook gives the history too. Press joining was patented in Europe in the late 1950s and came to the United States in the late 1990s.
Viega says its fittings join wet connections and press in four to seven seconds, and its Smart Connect feature lets an unpressed fitting leak during the pressure test so you can find it. The cost is up front: the tool and jaws.
Prep still matters. The handbook says the tube must be free of dents, deep scratches, dirt and grease, deburred inside and out, and marked for insertion depth.
Viega’s submittal sets the limits. ProPress goes only on copper tube to ASTM B88 or B75, and Types K, L and M all work. Soft copper is limited to ½ to 1¼ inch. Hard copper runs ½ to 4 inch.
Inside each fitting is a peroxide-cured EPDM seal. Viega rates the system at 300 psi operating and 600 psi test, from 0 to 250°F, with NSF 61 and NSF 372 listings. Its instructions say not to use oils or lubricants on the fitting.
Smart Connect has its own test window. Water at 15 to 85 psi, or air at ½ to 45 psi, finds an unpressed fitting. After that passes, Viega’s manual allows a test up to 600 psi with water or 200 psi with air.
Those are maximums, not required test pressures, and Viega warns that testing with air can be dangerous at high pressures. Viega says Smart Connect doesn’t replace the code test, so follow the test method and pressure your local code calls for.
The tool listed here is RIDGID’s RP 251 kit 78148, with ProPress jaws from ½ to 1¼ inch. RIDGID’s listing gives up to 140 presses per charge on its 12V battery, a 360° head swivel, LED lights, and over 60,000 press cycles with no scheduled maintenance. The in-line body and forward trigger are built for one-handed pressing overhead.
| Choose it if | Skip it if |
|---|---|
| You make a lot of joints, work in occupied buildings or tight ceilings, or can’t get a line dry. | You only fix a joint a year. A torch, flux and solder cost far less than a press kit. |
Key specs: 300 psi (Viega); 0–250°F; EPDM seal; Wet lines OK; 50-yr fitting warranty (Viega). On Amazon: RIDGID RP 251 kit 78148, ½–1¼ in. ProPress jaws. The Viega 78047 ½ in. coupling is a reference, shown for comparison only.
| Strengths | Trade-offs |
|---|---|
| Highest pressure rating: 1,090 psi at 100°F for ½–1 in. 95/5, per the CDA | Hard on wet lines: the CDA says soldering under wet conditions can be very difficult |
| Low startup cost | Open flame: fire risk near framing and finishes |
| Fittings are cheap and everywhere | Slower per joint: clean, flux, heat, solder, cool |
Soldering is still a great joint when it’s done right. Its 95/5 tin-antimony joint rating is 1,090 psi at 100°F for ½ to 1 inch; the tube, fittings and code still limit the system.
The handbook’s sequence comes from ASTM B828: measure and cut, ream, clean, flux, assemble and support, heat, apply solder, cool and clean, then test. Most soldering happens at about 350 to 600°F.
The fit is tight on purpose. The gap between tube and fitting is about 0.004 inch, and capillary action works best between 0.004 and 0.006 inch. Sand off too much copper and the fit gets loose, which the handbook says can crack the solder under stress or vibration.
The catch is process. Clean the copper bright, brush on a thin coat of B813 flux, heat the tube then the fitting, and feed solder until it fills. The handbook warns that overheating burns the flux and stops the solder. For the details, see solder and flux for copper.
Two rules people skip. A fluxed joint must be finished the same day, not left overnight. And the joint should cool on its own, since shock cooling with water may stress it. Wipe the flux off after, because too much flux residue can corrode the tube.
For drinking water, solder must be lead-free: no more than 0.2% lead under the Safe Drinking Water Act.
The consumables listed here fit that job. Oatey’s 22017 is 95% tin and 5% antimony, melts from 450 to 464°F, and is listed for drinking water lines. LA-CO’s 22194 flux meets ASTM B813 with no zinc chloride, washes out with water so it won’t leave residue in the piping, and meets NSF/ANSI 61 for potable water.
The handbook’s flux estimate is about 2 ounces per pound of solder. The 4 ounce LA-CO jar pairs with roughly 2 pounds of wire.
| Choose it if | Skip it if |
|---|---|
| You already own a torch, do a few repairs a year, and can drain the line. | The line won’t drain, or you’re working where a flame isn’t allowed. |
Key specs: 1,090 psi at 100°F; 505 psi at 200°F; Lead-free (95/5); ASTM B32 / B813. On Amazon: LA-CO 22194 flux, ASTM B813, 4 oz, Bernzomatic TS8000 trigger-start torch.
| Check | Press | Solder | Ahead |
|---|---|---|---|
| Heat at the joint | None | Open flame | Press |
| Wet lines | Joins wet connections (Viega) | Very difficult wet (CDA) | Press |
| Time per joint | 4–7 s press (Viega), plus prep | Clean, flux, heat, solder, cool | Press |
| Rated pressure, ½–1 in. | 300 psi (Viega); 200 psi general | 1,090 psi at 100°F (95/5) | Solder |
| Startup cost | Press tool and jaws | Torch, flux, solder | Solder |
| Finding a missed joint | Smart Connect leaks during the test | Visual check and pressure test | Press |
| Prep needed | Square cut, deburr, clean, mark depth | Square cut, ream, clean, flux | Even |
| Drinking water | NSF 61 fittings | Lead-free solder and flux only | Even |
| Size | 95/5 at 100°F | 95/5 at 150°F | 95/5 at 200°F | 95/5 at 250°F | Press-connect, general |
|---|---|---|---|---|---|
| ⅛–1 in. | 1,090 psi | 625 psi | 505 psi | 270 psi | 200 psi (½–4 in., 0–250°F) |
| 1¼–2 in. | 850 psi | 485 psi | 395 psi | 210 psi | 200 psi |
| 2½–4 in. | 705 psi | 405 psi | 325 psi | 175 psi | 200 psi |
Solder’s rating falls fast as the water gets hotter. At 250°F, a 2½ to 4 inch 95/5 joint is rated 175 psi, under the 200 psi general press-connect figure. The handbook says press ranges should be confirmed with the fitting maker, and Viega’s own is 300 psi.
At 150°F, ½ to 1 inch 95/5 joints are still rated 625 psi. The gap between the two methods shows up at the hot end of the table and in the bigger sizes.
| Lead-free solder (½–1 in.) | 100°F | 150°F | 200°F | 250°F |
|---|---|---|---|---|
| 95-5 tin-antimony (Sb5) | 1,090 psi | 625 psi | 505 psi | 270 psi |
| Alloy HB | 1,035 psi | 710 psi | 440 psi | 430 psi |
| Alloy E | 710 psi | 475 psi | 375 psi | 320 psi |
All three are lead-free and allowed on drinking water. The old 50-50 tin-lead is not: the 1986 Safe Drinking Water Act amendment bans solder over 0.2% lead in potable systems. Above 250°F, or where the highest joint strength is needed, the handbook points to brazing instead.
| Step | Press (handbook §11 and Viega) | Solder (handbook §7) |
|---|---|---|
| Cut | Square, without deforming the tube | Square, without deforming the tube |
| Deburr | Inside and outside, then chamfer the end so it won’t cut the seal | Ream to the full inside diameter; take off outside burrs |
| Clean | No dents, deep scratches, dirt, oil or stamped print lines | Abrade tube and fitting cup until bright |
| Before joining | Check the EPDM seal is there and undamaged; no oils or lube | Thin, even coat of ASTM B813 flux with a brush, not fingers |
| Insert | Mark the depth; push to the stop with a slight turn | Seat the tube against the cup with a slight twist |
| Join | Jaw on the bead at 90°; pull the trigger to start the press cycle | Heat tube, then cup; feed solder from the bottom, overlapping |
| Finish | Insertion mark still visible | Cool naturally; wipe off flux; flush the system |
| Test | Smart Connect range, then the code test | The code test |
Both joints start with the same prep: cut, deburr, clean. Press then skips the heating, soldering and cooling. Solder adds a same-day rule: a fluxed joint can’t wait until tomorrow.
| Tube size | ProPress minimum insertion | ProPress minimum gap between fittings | Solder fitting cup depth |
|---|---|---|---|
| ½ in. | ¾ in. | 0 | 0.500 in. |
| ¾ in. | ⅞ in. | 0 | 0.750 in. |
| 1 in. | ⅞ in. | 0 | 0.910 in. |
| 1¼ in. | 1 in. | 7/16 in. | 0.970 in. |
| 1½ in. | 1 7/16 in. | ⅝ in. | 1.090 in. |
| 2 in. | 1 9/16 in. | ¾ in. | 1.340 in. |
Viega warns that the wrong insertion depth may give an improper seal, so mark it every time. From 1¼ inch up, ProPress also needs a minimum gap between fittings, or the jaw can’t seat. That matters on tight manifolds where solder fittings could sit closer together.
Measure the tube length with the depth in mind. The handbook says a tube cut too short won’t reach the bottom of the cup and can’t make a proper joint.
| Item | ProPress copper fittings | Soldered joint |
|---|---|---|
| Drinking-water listing | NSF 61 and NSF 372, CSA Low Lead | Depends on the solder; lead-free required on potable lines |
| Code listings | IAPMO Z1117, ICC-ES LC1002, ABS | Joint made to ASTM B828 practice |
| Tube | ASTM B88 Types K, L, M, or B75 | ASTM B88 Types K, L, M |
| Seal or filler | Peroxide-cured EPDM | 95/5, Alloy E or Alloy HB solder |
| Warranty | 50-year limited, only with Viega-compatible tools | No system warranty; each part has its own |
The ProPress warranty has a catch worth reading. Viega says it applies only when the fittings are pressed with tools compatible with Viega systems. A jaw that isn’t compatible with Viega systems can leave you without that coverage, so check compatibility before you buy one.
A soldered joint has no single maker behind it. The fitting, the solder and the flux each come from a different company, and the joint is only as good as the prep and heat.
| Spec | RIDGID RP 251 (78148), per its listing |
|---|---|
| Copper and stainless | Up to 1¼ in. |
| PEX | Up to 1½ in. |
| Carbon steel | Up to 1 in. |
| Presses per charge | About 140 |
| Battery | 12V |
| Service | Over 60,000 cycles with no scheduled maintenance |
| Head | Rotates 360° |
The 1¼ inch limit decides a lot. Viega’s hard copper fittings go up to 4 inches, but a 12-volt tool like the RP 251 stops at 1¼. For 1½ and 2 inch work you need a larger press tool and jaws, which costs more again.
For a house, 1¼ inch covers most water lines. If your job has a 2 inch main, price the bigger tool before you decide press is cheaper.
| Need | Press | Solder |
|---|---|---|
| Cutter | Yes, square cut | Yes, square cut |
| Deburring tool | Yes, inside and outside, plus chamfer | Yes, ream to full ID |
| Cleaning | Wipe clean; no print lines | Sand cloth and fitting brush to bright metal |
| Heat source | None | Air-fuel torch, or an electric resistance tool |
| Consumables | Fittings only | Solder, flux, flux brush, rags |
| Press tool and jaws | Yes, sized to each pipe | No |
| Fire safety | No open flame at the joint; site, electrical and pressure-test safety still apply | Shield near framing; follow ANSI/AWS Z49.1 |
The cutter and deburring tool are shared. If you already solder, you own half the press kit. The new money is the press tool and a jaw for each size, and after that you stop buying gas, solder and flux.
| Tube size | Solder per 100 joints (0.010 in. gap) | Flux at 2 oz per lb of solder |
|---|---|---|
| ½ in. | 0.261 lb | About 0.5 oz |
| ¾ in. | 0.548 lb | About 1.1 oz |
| 1 in. | 0.856 lb | About 1.7 oz |
| 1¼ in. | 1.115 lb | About 2.2 oz |
| 1½ in. | 1.480 lb | About 3.0 oz |
| 2 in. | 2.380 lb | About 4.8 oz |
These are the handbook’s Table 14.10 figures for ⅛ inch (No. 9) wire solder. They already include a 100% allowance for waste and loss, and the handbook says real use depends on workmanship. The flux column is the handbook’s rule of 2 ounces per pound, worked out per row.
For a house repipe with mostly ½ and ¾ inch joints, a 1 pound spool goes a long way. A 4 ounce flux jar covers about 2 pounds of solder. Press uses none of this: the seal is already in the fitting.
| Method | Mistake | What the source says |
|---|---|---|
| Press | Fitting with a missing seal | The handbook shows a missing O-ring as the thing to check for |
| Press | Tube not fully inserted | The mark must still show after pressing |
| Press | Print lines left on the tube | Viega: tube must be free of stamped print lines |
| Press | Oil or lube on the fitting | Viega: don’t use oils or lubricants |
| Solder | Overheating | Burns the flux, so solder won’t enter the joint |
| Solder | Too much flux | Residue can corrode, in extreme cases through the wall |
| Solder | Loose fit | Solder can crack under stress or vibration |
| Solder | Shock cooling with water | May stress the joint |
| Situation | What the handbook says |
|---|---|
| Water won’t drain from the line | Soldering wet can be very difficult; flared, press and push joints are preferred |
| Fire hazard, torch not allowed | Flared joints may be required; press needs no heat or flame |
| Flame is a concern, but you want solder | Electric resistance soldering tools heat with electrodes, not a flame |
| Over 250°F, or highest strength | Use brazing filler metals |
Air-fuel torches burn acetylene or LP gas, and the handbook points to ANSI/AWS Z49.1 for open-flame safety. If you do solder near framing, a solder-cup valve should be partly open and the heat kept mostly on the tube, per the handbook.
| Joint type | Sizes | Pressure | Temperature |
|---|---|---|---|
| Press-connect, general piping | ½–4 in. | 0–200 psig | 0–250°F |
| Press-connect, high-pressure HVACR | ¼–1⅛ in. | 0–700 psig | −25 to 300°F |
| Push-connect | ½–2 in. | 0–200 psig | 0–250°F |
The HVACR press line is a different system. The handbook says its fittings, jaws and tools aren’t interchangeable with standard low-pressure press fittings, so a plumbing ProPress jaw isn’t for a refrigerant line. Push-connect carries the same general rating as press with no press tool. The handbook adds that real ranges should be confirmed with each fitting maker.
Most plumbers end up owning both. Here’s how the choice usually falls.
The CDA says soldering under wet conditions can be very difficult and press joints are preferred there. Viega says ProPress joins wet connections. See can you press a wet line.
Occupied buildings, finished ceilings and tight framing. The handbook’s main point for press is no heat or open flame.
A torch, flux and solder cost a fraction of a press kit, and the joint is rated higher.
Square cut, deburred and clean. Both methods fail on dirty or damaged copper. See my deburring tool picks.
For house water, yes. Viega rates ProPress at 300 psi and 0 to 250°F with a 50-year fitting warranty. A 95/5 soldered joint is rated higher on paper, up to 1,090 psi at 100°F for ½ to 1 inch.
The tool and jaws cost a lot up front, the fittings cost more than solder fittings, and the jaws need room around the joint. Each joint also depends on the EPDM seal being present and the fitting fully inserted.
Many use press fittings for repairs and remodels because there’s no flame and wet lines aren’t a problem. Soldering is still common, especially where a torch is already on the truck.
Viega backs its copper press fittings with a 50-year warranty. Soldered joints have no single maker’s warranty, but properly made ones are rated higher and have a long record.
Yes with ProPress. Viega says it lets installers join wet connections. The CDA says soldering under wet conditions can be very difficult.
The press itself takes four to seven seconds, per Viega, against heating, soldering and cooling a sweat joint. The cutting, cleaning and depth marking take the same time either way. Press also works on a wet line, per Viega, where the CDA says soldering can be very difficult.
A lead-free solder: 95-5 tin-antimony, Alloy E or Alloy HB. The Safe Drinking Water Act bans solder over 0.2% lead in drinking water systems.
Yes, from ½ to 1¼ inch, per Viega. Hard copper can be pressed from ½ to 4 inch.
To find unpressed fittings with Smart Connect, Viega says water at 15 to 85 psi or air at ½ to 45 psi. Viega lists 600 psi with water or 200 psi with air as maximums after that passes, not required test pressures, and warns that testing with air can be dangerous at high pressures. Your local code sets the required test; a water test is the safer default.
Viega’s minimum insertion depth is ¾ inch for ½ inch tube and ⅞ inch for ¾ and 1 inch. Mark it before you insert the tube.
No. Viega’s listing says press eliminates solder and flux, and its instructions say not to put oils or lubricants on the fitting.
The handbook says most soldering is done at about 350 to 600°F. Oatey’s 95/5 melts from 450 to 464°F.
The Copper Tube Handbook says soldering under wet conditions can be very difficult, and it names flared, press and push joints as the preferred choice.
Not the plumbing line. The handbook says high-pressure HVACR press fittings, jaws and tools are a separate system and aren’t interchangeable with standard press fittings.
Viega’s 50-year limited warranty on ProPress copper fittings applies only when they’re pressed with tools compatible with Viega systems.
RIDGID lists about 140 presses per charge for the RP 251 on its 12V battery, and over 60,000 cycles with no scheduled maintenance. It presses copper up to 1¼ inch.
Links go to listings sold by Amazon.com.
I’m Isaac Daniels, a licensed journeyman plumber in Georgia. The ratings here come from the Copper Development Association’s handbook and Viega.
In my 7 years of experience, these are the products I’d install.